Sunday, January 1, 2017

How to Make a DIY Ingot Mold for Aluminum, Lead or Zinc Casting

Difficulty Level (Easy, Medium, Hard, Insane):
Easy

Process:
I've used a square corn bread muffin pan to cast my left over aluminum but because the material is so thin, the 640 degree (C) molten metal warped the muffin pan quite badly to the point where it was hard to get the ingots out so I decided I was going to make a more permanent solution.

My brother in law generously gave me 3 feet of 2.500" by 1.500" square tubing (1/8" thick) so I took my metal band saw, set the vise to about 3 degrees and cut 8 pieces at 4" long.

After deburring the edges, I used my angle grinder to cut off the top piece of the square tubing (the end where the tubing was welded together. Then I used a grinding wheel to grind off any protruding metal that could prevent the ingots from sliding out.

Then, I used the vise and a 2.500" diameter piece of brass to press it into the c-channel pieces to widen out the top.

After that, I took some 1.500" wide by 1/8" thick flat bar, cut 16 pieces at 2.500" wide and welded them to each side of the square tubing pieces.

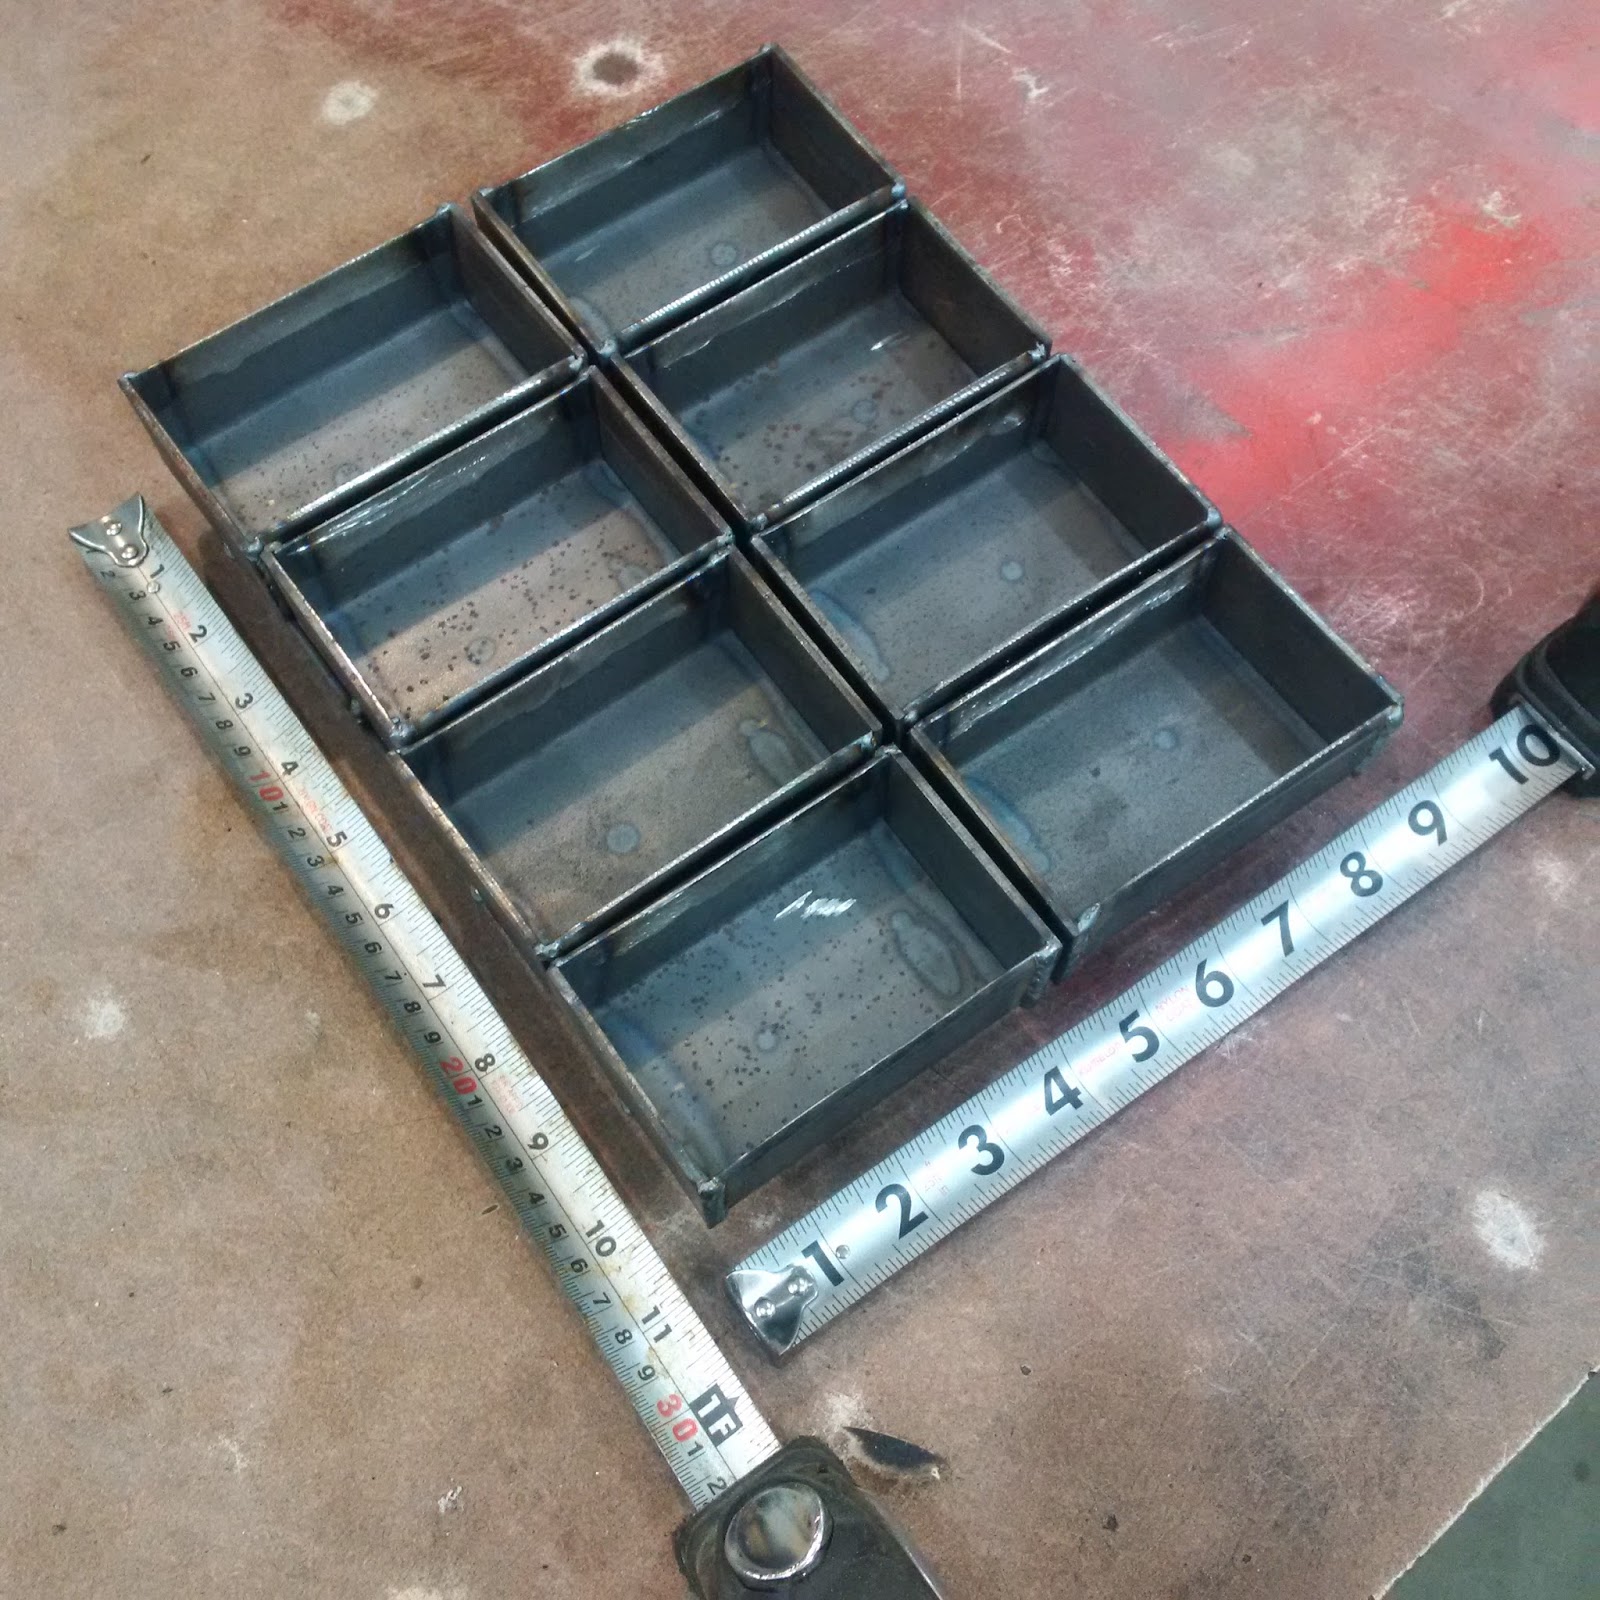
Lastly, I used some 1" angle iron to weld all the 8 finished individual ingot molds together into one unit.

Videos:


Pictures:
Some zinc ingots made using a square corn bread muffin pan

Some aluminum ingots made using the same corn bread muffin pan


The muffin pan taking its toll because the metal is so thin

The bottom of the muffin pan quite heavily warped

Starting out with some 2.500" by 1.500" square tubing

Cutting 4" pieces with a 3 degree angle on the sides

Welding some flat bar on the sides

All 8 molds welded and laid out to connect together

Using some 1" angle iron to tie the individual molds together

Reinforcing the outside with some more 1" angle iron

The finished ingot mold

Trying it out with some lead

Thirty four-pound ingots later

The ingots turned out really nice

Another view of the lead stack
My stash
Cutting up two square bars for the handles

After I bent and welded the handles to the ingot mold

Tools:

Metal band saw
Measuring tape
Marker
Square
Angle protractor
Angle grinder
Eye and ear protection
Belt sander
MIG welder
DIY MIG welder cart
Aluminum foundry
Foundry burner

Materials:
32" of 2.500" by 1.500" square tubing
28" of 1" angle iron
20" of 3/8" by 3/8" square iron bars

Cost:
$0.00

Time:
4 hrs

Savings:
$50

Conclusion:
Ah, it's so nice to have some decent ingots! Yes, go ahead, roll your eyes at me, Melanie!

Fixing Hinge for Samsung SCX-4828FN Scanner Lid

Difficulty Level (Easy, Medium, Hard, Insane):
Easy

Process:
My wife told me that while she was ferociously photocopying home schooling curriculum she broke the lid off our all-in-one photocopier (Samsung SCX-4828FN) so I had a look and fond that she had indeed broken one of the injection-molded plastic hinges.

After taking it off the photocopier I had a closer look at it and realized that gluing was out of the question, plastic welding wouldn't work either and the only thing that jumped out at me was to take a piece of aluminum and machine one from scratch.

However, the time this would take was not sitting right with me so I did some searching online and actually found a replacement hinge on ebay, but was shocked that the price plus shipping was close to $50 bucks.

After some more thinking I came up with a way to do it that wasn't going to take too much time and would still be solid enough to never ever break again.

Basically, I took a strip of 18 gauge sheet metal and bent it around the plastic hinge, riveted it to the bottom and each side and then drilled two holes at the appropriate height from the bottom.

It actually turned out quite easy to do. It still took me about two hours, but now I know that that hinge will never break again, no matter how savagely she works that machine.

The last thing I had to do was to take a dremel and widen the plastic hole in the photocopier to make room for the extra width of the hinge and voila, all done.

Videos:

 
Pictures:
The broken hinge

The way it's supposed to look (picture from $50 ebay hinge)

A piece of 18 gauge steel I cut to size on the metal band saw

After the piece of metal was bent to its proper shape

Another view

Test fitting the bracket to the broken hinge

Front view

Putting a rivet at the bottom of the hinge

The finished hinge

Another view

Another view

Taking the trim off to widen the hole for the wider hinge

A few hidden screws under the control panel

The hinge installed to the lid, but before putting it onto the printer base

Widening the hole in the plastic trim

The installed hinge

Another view

Tools:

Metal band saw
Hammer
Vise
Drill
Digital calipers

Materials:
6" of 3/8" wide, 18 gauge steel
3 rivets

Cost:
$0.00

Time:
2 hrs

Savings:
$50

Conclusion:
It works great. Another notch on the belt!

Saturday, December 10, 2016

Contemporary Nativity Scene

Difficulty Level (Easy, Medium, Hard, Insane):
Easy

Process:
I came across a picture online of an Ultra Modern Nativity Scene and was quite intrigued with the set. It was designed by Sebastian Bergne but unfortunately, he only made 250 sets and paying $140 (CAD) for a bunch of painted blocks is just a little bit too much for my budget.

Regardless, the longer I looked at the pictures, the more I started to like it and decided I was going to make a set for my wife. The design is so simple and the only real challenge in reverse engineering was to come up with the proper dimensions, so here they are (H x W x D):

Joseph, wise men, Shepherds: 4" x 1" x 3/4"
Mary: 2-1/2" x 2" x 3/4"
Jesus: 1-1/2" x 2" x 3/4"
Angel: 4" x 3/8" x 3/4"
Stable frame outside: 5-3/8" x 9-7/8" x 1"
Stable frame inside: 4-1/8" x 8-1/2" x 3/4"
Stable back wall: 4-1/8" x 8-1/2" x 1/4"

The material I used for the blocks was solid white oak, the back wall of the stable was oak laminated particle board and the frame of the stable was made with solid pine.

After I cut the strips oversize, I put them through my planer and cut them to length on the chop saw. Then came the fairly time-consuming process of sanding the pieces on the belt sander.

To paint the pieces, I drilled a small hole into the bottom of each of the blocks and hammered a nail into it, then I took a 3 foot piece of 2x2 and drilled a bunch of holes (the same size as the heads of the nails) at 2" intervals. That way, I could paint the underside of the block, then stick the nail into the hole of the 2x2 and paint the sides without having to touch the pieces. Also, I was able to do it all in one coat and it could dry all around.

After the pieces were dry I put a thin clear coat over it all and let it dry over night. All that was left to do in the morning was to assemble it and present it to my wife.

Pictures:
Planing the boards to size

The planed boards

Close-up of the oak

I had to sharpen my chop saw blade

Using a diamond sharpening blade it works great

A view from a different angle

The sharpened carbide tips

After the oak pieces were cut to size

My Jerry-rigged setup for the belt sander. Soon I'll have a bench top version but I still need to fix that one (blog to come)

Some of the sanded pieces

Doing a test setup of the nativity scene

The nails at the bottom of each piece

Standing them up on a 2x2 so they can dry

Starting the painting process

Another angle

About half-way done with the painting

Painting is all done


Testing to make sure the stable/box is the right size

The finished (but not yet clear coated) nativity set

Test setup

Clear coating the stable

Clear coating the other pieces

All done, waiting for the clear coat to dry

The finished set

Tools:
Wood planer
Table saw
Chop saw
Belt sander
Hammer
Measuring tape
Ear & eye protection
Pencil
Sand paper

Materials:
24" of 1" by 3/4" white oak
4" of 2" by 3/4" white oak
30" of 1" by 3/4" solid pine
6" by 9" piece of 1/4" oak laminated particle board
Tole paint
Four 2" nails
Wood glue

Cost:
$0.00 (I had all the materials in the shop already)

Time:
9 hrs

Savings:
$112.99

Conclusion:
Success. I hope it will last.

Followers